Ce Certified Double Barbed Wire Factory
Double barbed wire consists of two parallel steel strands twisted together, with uniformly spaced barbs formed by cutting and pressing the wire to create sharp protrusions on both sides. This
CE Certified Double Barbed Wire – Factory Overview
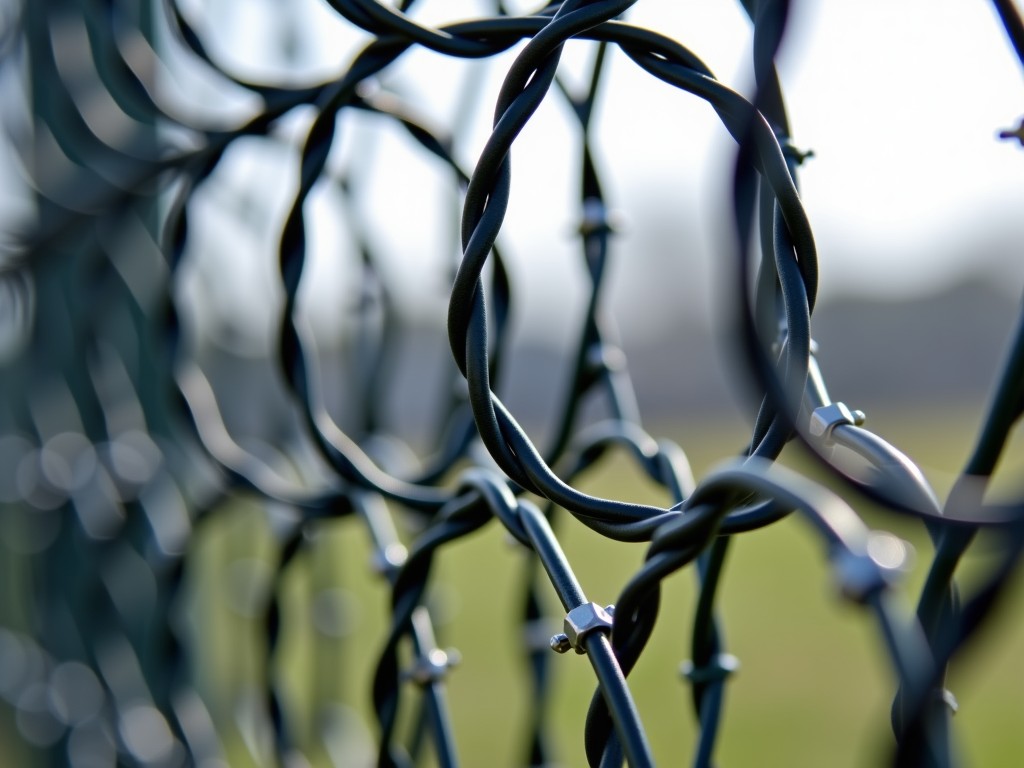
Double barbed wire consists of two parallel steel strands twisted together, with uniformly spaced barbs formed by cutting and pressing the wire to create sharp protrusions on both sides. This geometry increases tensile resistance and provides a more effective deterrent compared with single‑strand barbed wire, making it suitable for high‑security perimeters where mechanical strength and puncture resistance are critical.
Achieving CE marking requires the product to meet the essential health and safety requirements of the European Construction Products Regulation (CPR) and, where applicable, the Machinery Directive. Conformity is shown through type testing, factory production control, and a technical dossier containing test reports on tensile strength, elongation, corrosion resistance, and barb sharpness.
Material Selection
Production of the core wire begins with high‑carbon steel grades such as C1080 or C1090, which attain the needed hardness after cold drawing. The steel is drawn to the target diameter and then twisted in opposite directions to create the double‑helix core, raising yield strength and ensuring uniform tension distribution.
- Hot‑dip zinc coating (200‑350 g/m²) for general outdoor exposure
- Zinc‑aluminum alloy coating (Zn‑5%Al) for enhanced corrosion resistance in marine environments
- Stainless steel core (AISI 304 or 316) where chemical exposure or aesthetic requirements demand non‑ferrous material
Manufacturing Process
After drawing, the two strands are fed into a counter‑rotating twisting head that imparts a lay length of approximately 100 mm. The twisted pair then passes through a barb‑forming station where dies cut and press the wire to create barbs on both sides of each strand. The barb height is typically 1.2 mm to 1.8 mm, and the barb angle is set to 45° relative to the wire axis to optimize penetration resistance.
Immediately after forming, the wire enters a hot‑dip galvanizing bath where immersion time and temperature are regulated to obtain the prescribed coating mass. Following cooling, the wire undergoes inline tension testing and visual inspection before winding onto reels or placement in protective sleeves for shipment.
Certification & Compliance
Under the Construction Products Regulation (EU) No 305/2011, CE marking for fencing products is issued. Manufacturers must maintain a Factory Production Control (FPC) system that includes regular testing of tensile strength, elongation, coating adhesion, and barb sharpness, with test results retained for at least ten years and made available to notified bodies on request.
Besides CE marking, the product can comply with ISO 1461 for hot‑dip galvanizing, ASTM A121 for zinc‑coated steel barbed wire, and regional standards such as EN 10223‑3 for barbed wire fittings. Verification of compliance relies on third‑party laboratory reports accompanying each production batch.
Applications
Perimeter security: The dual‑strand configuration provides a higher moment of inertia, making the wire resistant to cutting and bending forces. When installed at a height of 2.0 m with a 45° over‑hang, the barbs create a continuous barrier that increases the time required for intrusion, which is a key metric in security risk assessments.
Livestock containment: The uniform barb spacing prevents animals from pushing through the fence while minimizing injury to hides. The galvanized coating ensures a service life exceeding 15 years in typical pasture conditions, reducing replacement frequency and associated labor costs.
Industrial site perimeter: In environments with occasional exposure to solvents or alkaline cleaning agents, a zinc‑aluminum alloy coating offers superior corrosion resistance compared with standard zinc, maintaining tensile strength above 1 200 MPa after five years of exposure per ISO 9227 salt‑spray testing.
Quality Control
Each production lot undergoes dimensional verification (wire diameter, barb spacing, lay length) using laser micrometers, mechanical testing (tensile strength, elongation) on a universal testing machine, and coating mass measurement via gravimetric methods. Barb sharpness is assessed with a standardized puncture probe that measures the force required to penetrate a 2 mm rubber substrate.
- Wire diameter tolerance ±0.05 mm
- Barb height 1.2 mm – 1.8 mm ±0.1 mm
- Tensile strength ≥1 200 MPa (sample size 5 per lot)
- Elongation at break ≥10 %
- Coating mass 200‑350 g/m² (X‑ray fluorescence)
- Barb penetration force ≥15 N
Customization Options
Customers can specify core diameter, barb spacing, coating type, tensile strength grade, and roll length to match project‑specific engineering drawings. The factory’s CNC‑controlled twisting and barb‑forming equipment allows rapid changeover between configurations without compromising dimensional consistency.
- Core diameter: 1.8 mm – 4.0 mm
- Barb spacing: 50 mm – 200 mm
- Coating: hot‑dip Zn, Zn‑Al, or stainless steel
- Tensile strength grade: standard (1 200 MPa) or high (1 600 MPa)
- Roll length: 25 m – 300 m (custom spools available)
Packaging & Logistics
Finished coils are wrapped in UV‑stabilized polyethylene film, placed on wooden pallets, and secured with steel straps. For export shipments, additional corner protectors and moisture‑absorbent desiccant packs are included to prevent corrosion during transit. Pallet dimensions are standardized at 1.2 m × 1.0 m, allowing efficient container loading.
- Standard polyethylene wrap
- Vacuum‑sealed barrier bag for high‑humidity climates
- Wooden crate with internal bracing for heavy‑duty handling
- Labeling with batch number, CE marking, and QR code linking to test certificates
For technical datasheets, sample requests, or a project‑specific quotation, please contact our engineering team.
Request Quotation